


Sensor solutions for the confectionery and bakery industry
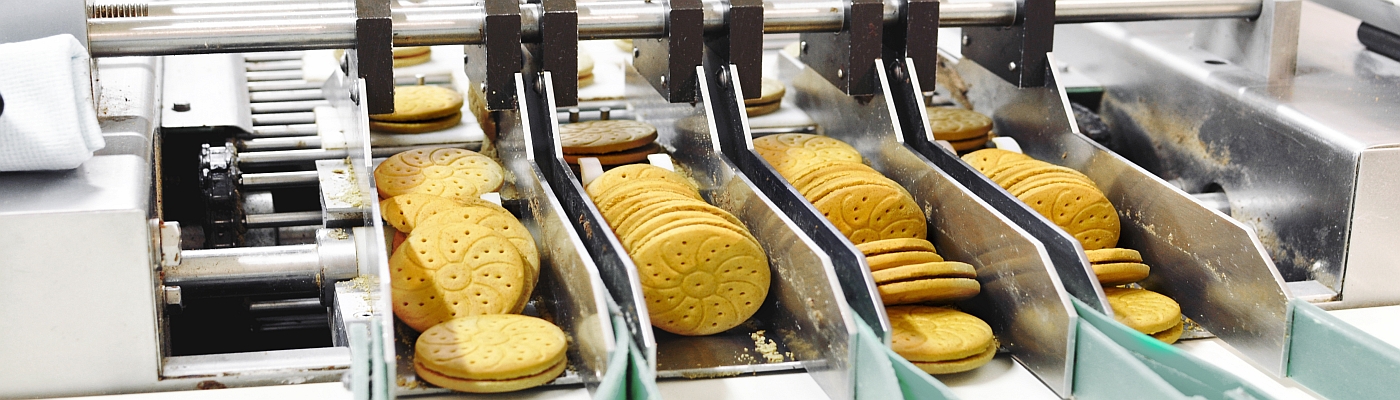
When it comes to automated packaging processes in the confectionery and baked goods industry, one thing is paramount: maximum flexibility. A wide variety of products are often processed and packaged on a single packaging line – in single-track systems depending on size, but primarily in multi-track systems. Accordingly, there is a need for sensors that can reliably detect a wide variety of products without requiring adjustments or additional settings.
Detection becomes particularly challenging when confectionery and baked goods are packaged in high-gloss or transparent films. The main challenges lie in reliable object detection from above – as is common in multi-track systems – and in ensuring a high degree of independence from the products’ color, shape, and material properties.
Sensor solutions along the processing and packaging lines
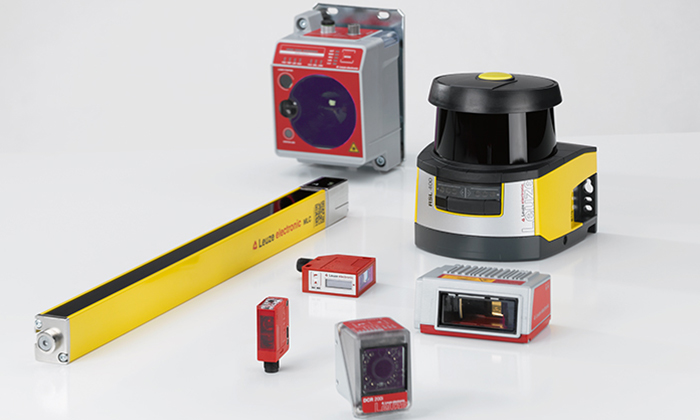
Our innovative sensor solutions are specifically designed to meet the demanding requirements of processing and packaging systems in the confectionery and baked goods industry. They enable reliable detection of products with complex shapes or challenging surface characteristics and ensure stable, reliable processes – even in multi-track systems.
In addition, modern sensor technologies enable the reliable detection of packaged products, even when transparent, high-gloss, or metallized films are used. For more demanding testing and inspection tasks, flexible image processing solutions are also available, enabling a wide range of verification and quality inspections directly within the process.
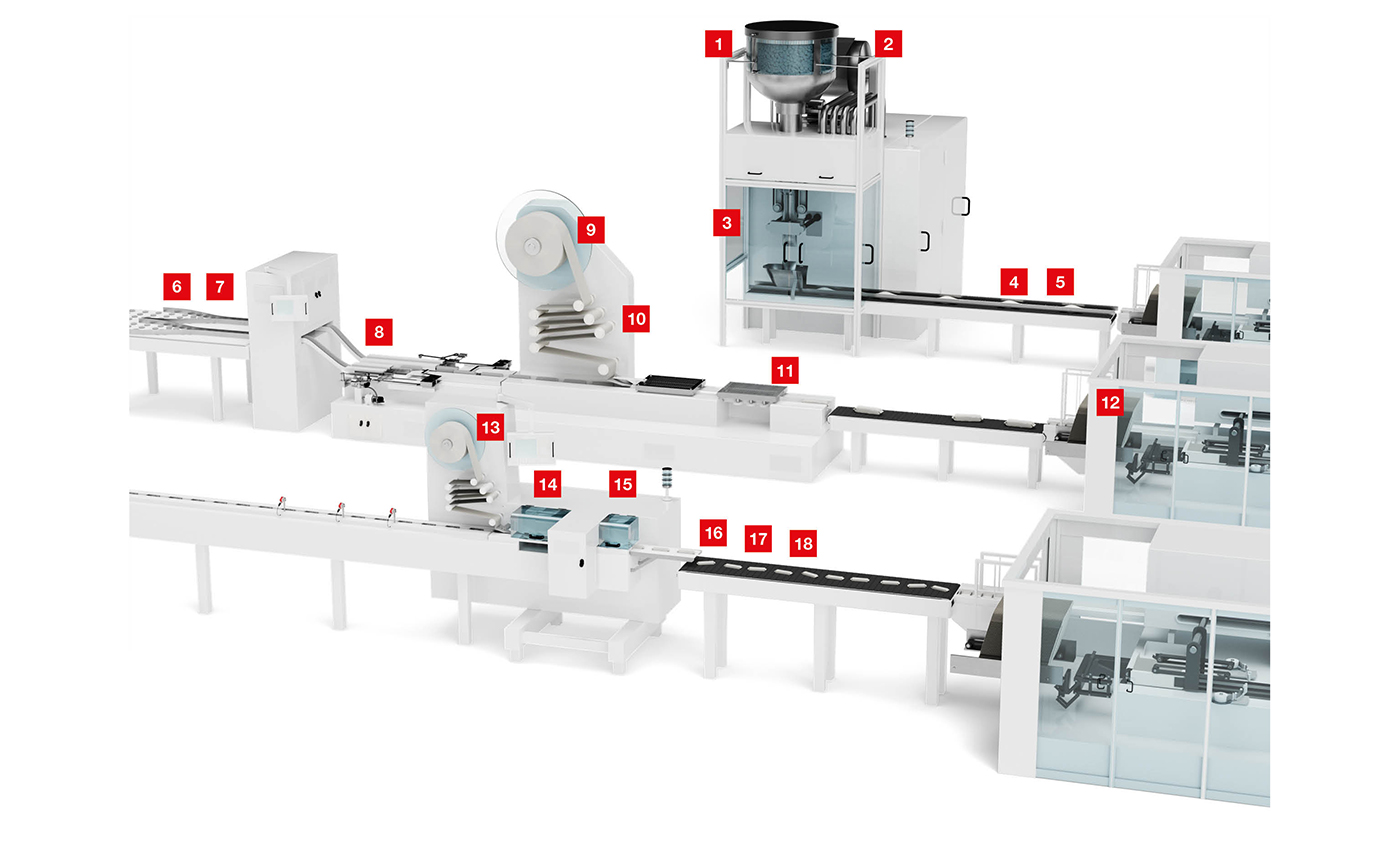
Applications in the packaging process for the confectionery and baked goods industry:
The applications throughout the process are as diverse as the products themselves – ranging from object transport and process monitoring to quality assurance and packaging materials.
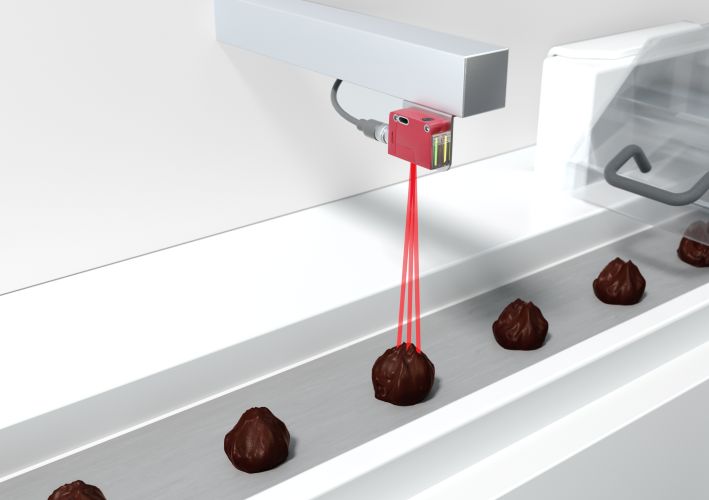

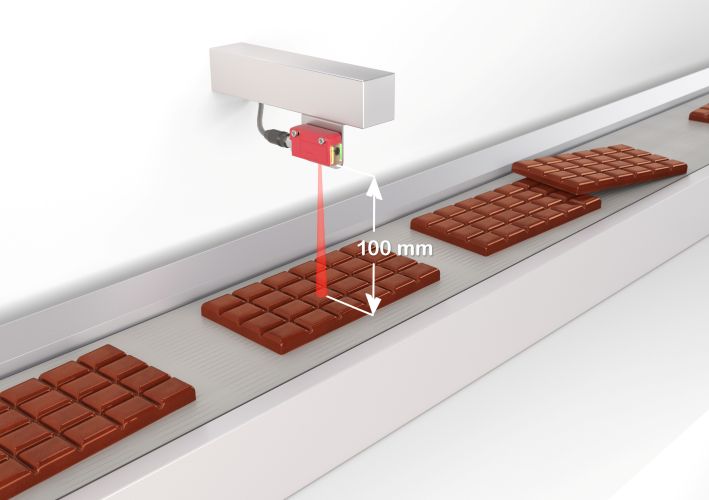
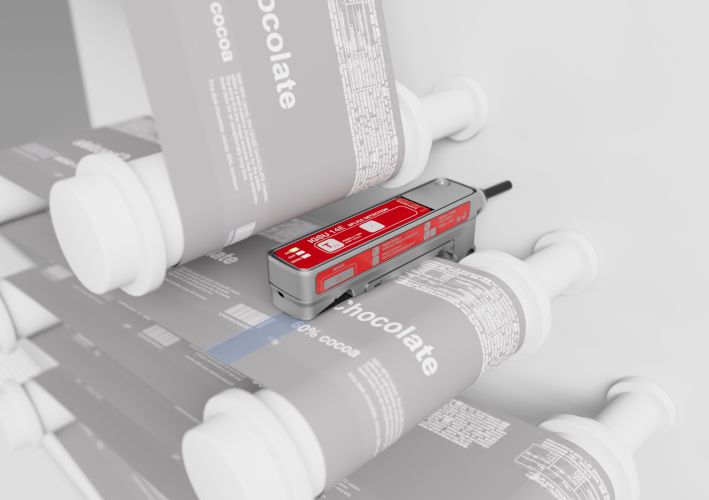
Applications for object transport
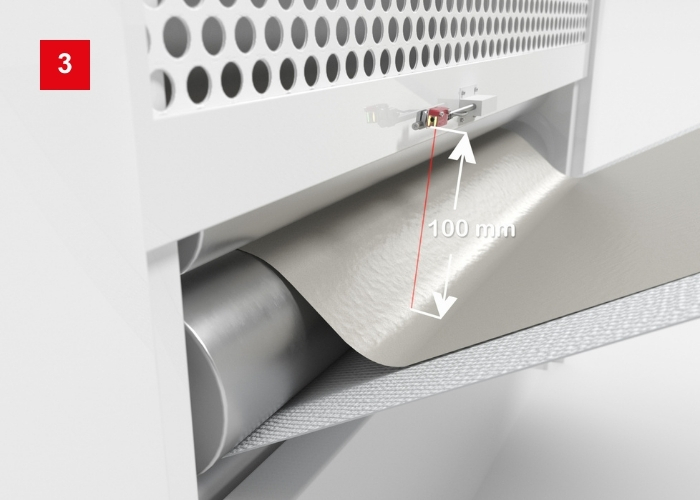
Dough loop control
Requirement:
Dough is rolled out in a machine and later processed into baked goods. The dough is precisely rolled out to a required thickness. A sensor monitors that the dough retains its shape unchanged when transferred to the conveyor belt. The distance between the dough and the sensor is used as the measured variable.
Solution:
The ODT 3C distance diffuse sensor is positioned at the output of the rolling machine above the dough loop and provides a distance value to the higher-level control. The measurement value is evaluated using the process data via IO-Link. In addition, diagnostic data is transmitted to the controller via IO-Link for Industry 4.0 purposes.
Detection of products on conveyor belts
Requirement:
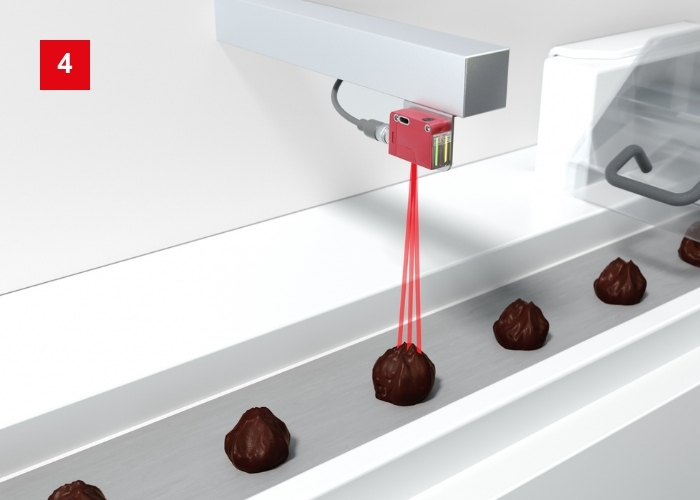
To control the buffer section, the front edges of the products on the conveyor belt must be reliably detected. The sensor must also detect products with challenging dimensions from very flat to very tall, in order to prevent machine downtimes due to incorrect detection.
Solution:
Due to its operating principle, the DRT 25C dynamic reference diffuse sensor reliably detects the entire range of products, from small and flat to tall and spherical. The single button teach function makes the DRT 25C easy to set up. Additional sensor functions can be controlled via the IO-Link interface.
Multiple-track object detection
Requirement:
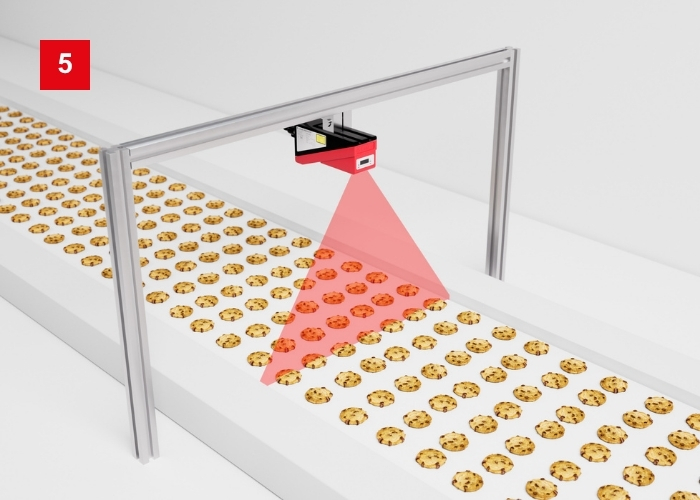
In the food industry, products are often transported between processes in multiple tracks. Detection of products for presence and/or completeness can only be done from above and should cover all tracks.
Solution:
The LRS 36 light-section sensors for object detection, the LES 36 for object measurement, and the LPS 36 for profile measurement detect various objects across a measurement field width of 600 mm. Missing products are thus easy to identify. The sensors output object position and height.
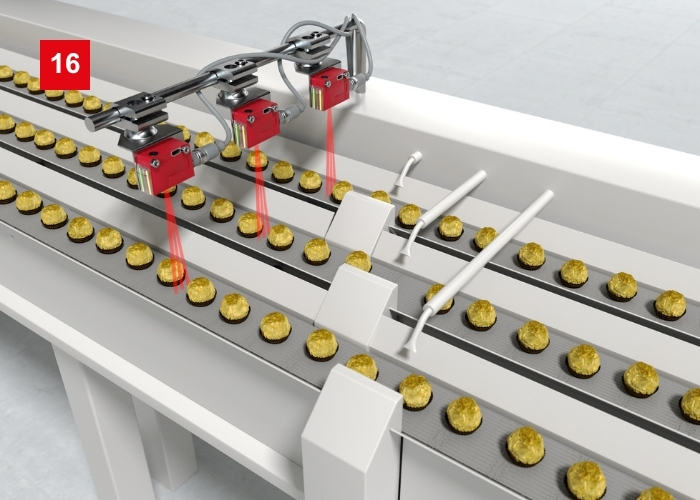
Detection of packaged products
Requirement:
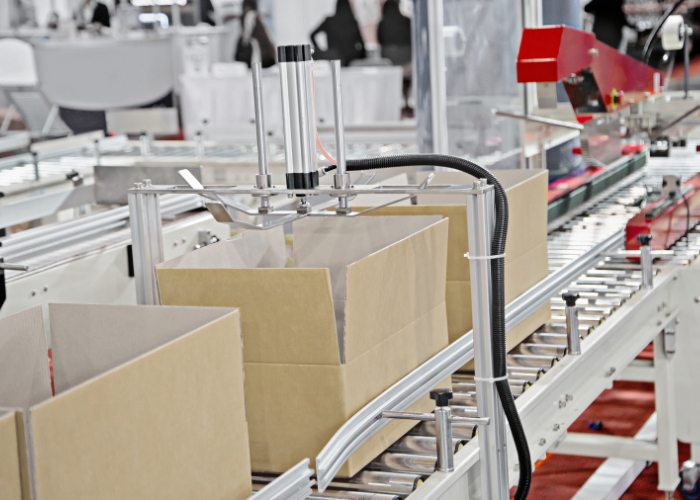
If several conveyor belts are arranged next to each other at a close distance, it is necessary to detect objects from above. In production plants, adaptations to sensors should ideally not be necessary during format changes to avoid downtimes.
Solution:
Using the conveyor belt as a reference and the processing of diffuse reflection and distance, the DRT 25C reference diffuse sensor detects all objects. One teach event during commissioning is sufficient – no adaptation is required for format changes.
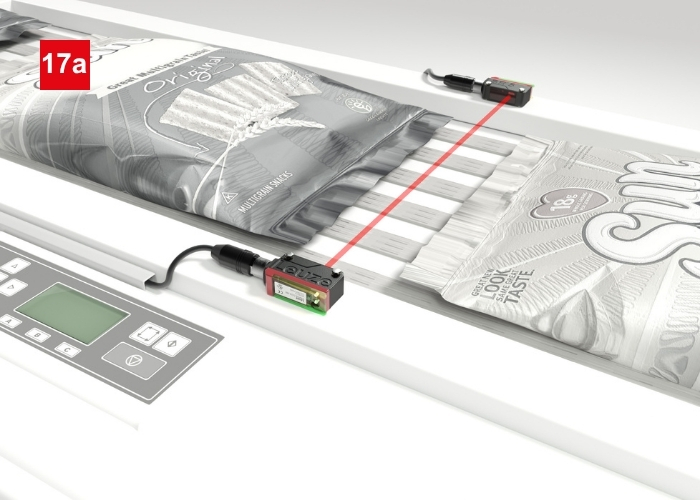
Detection of products on conveyor belts
Requirement:
At a food manufacturer, products are packed in high-gloss primary packaging. The packages are then transported further on a conveyor belt where they are to be reliably detected. Sensors with short response time can detect even small gaps between products.
Solution:
The sensors of the 5B series can be mounted horizontally on the conveyor line. The advantage of the throughbeam photoelectric sensor is the very high function reserve. This ensures reliable detection even with critical surfaces.
Process monitoring applications

Fill level monitoring
Requirement:
In confectionery production, numerous ingredients and additional items such as chocolate buttons, liquids, etc. are used. For continuous control of the provision of ingredients, the fill levels in the respective containers must be detected.
Solution:
The LCS capacitive sensors detect the fill levels of liquids or bulk materials in plastic or glass containers. The sensors detect through the container wall without coming into contact with the product. The position of the sensors defines a minimum and a maximum fill level.

Detection of residual quantities in empty molds
Requirement:
Before reusing empty molds, it must be ensured for a reliable production process that no residues are present in any of the molds.
Solution:
The LRS 36 light section sensor records a profile of the mold and provides a distance and position value for each measuring point along the laser line. The connected control evaluates "empty" or “residues in the mold". Alternatively, the IVS 1000i Simple Vision sensor with integrated image processing can be used.
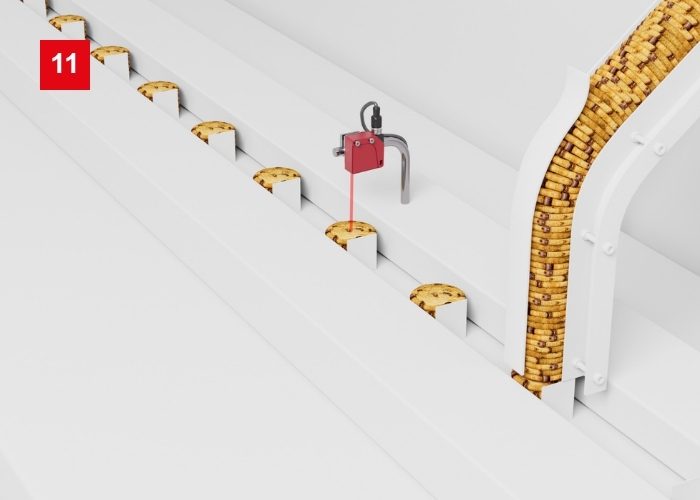
Product height verification
Requirement:
If several flat products are stacked on top of each other, the stack height must be monitored so as not to impair the subsequent packaging process. At the same time, the number of stacked products can be controlled.
Solution:
Thanks to their different measurement ranges and resolutions, the ODS measuring distance sensors are suitable for fill-level monitoring. Thanks to the configurable analog current or voltage output and the IO-Link interface, they can be easily adapted to the specific application.
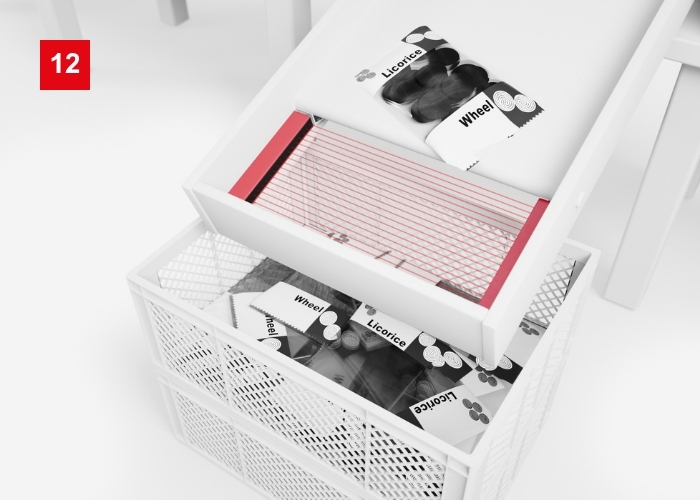
Ejection monitoring and product count
Requirement:
Defective or incomplete products are ejected without sorting or alignment on a packaging machine. Switching light curtains can detect these products. Alternatively, a fast switching light curtain can be used at the outlet of the machine to count the properly packaged products.
Solution:
The CSL 710 switching light curtain is suitable for monitoring larger ejection openings thanks to its various lengths and resolutions. The compact CSL 505 light barrier is a space-saving solution for simple applications. The CSR 780 retro-reflective light curtain is suitable for fast object counting due to its short response time.
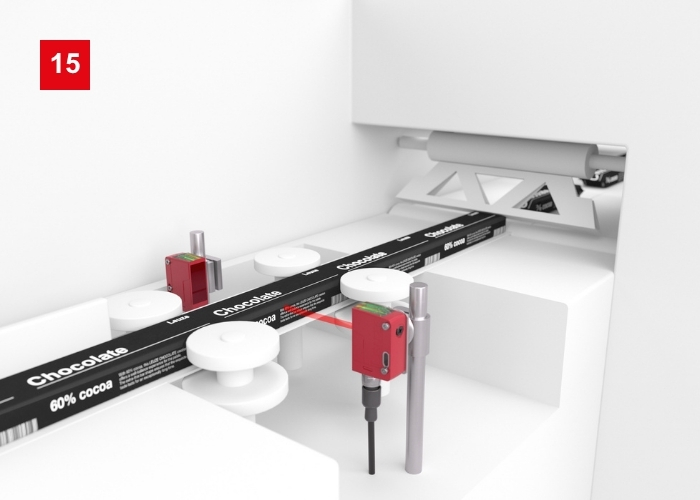
Detection of packaging content
Requirement:
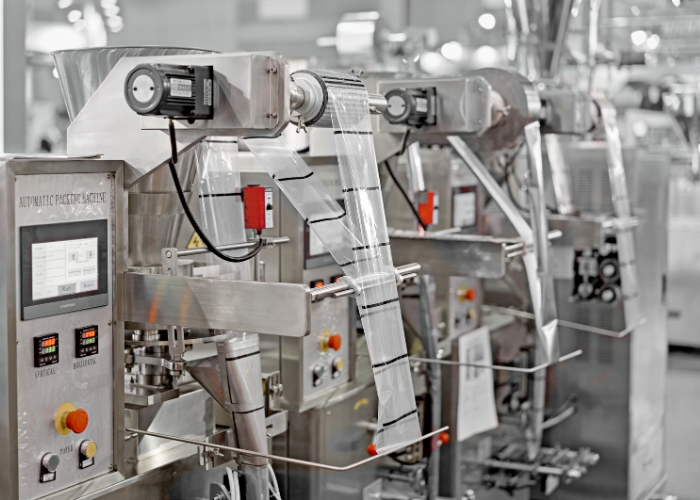
Chocolate bars, for example, are packed in film in a horizontal packaging line. The packaging film mostly has a colorful print and is opaque. To ensure that sealing occurs at the correct point on the film tube, the front edge of the bar located inside the film tube needs to be reliably detected.
Solution:
The high-performance super und high power LS25CI.XXR und LS25CI.XR throughbeam photoelectric sensors effortlessly transilluminate most metallized and dark-colored films. Even in the sealed film tube, the front edges of the products in the packaging are reliably detected.
Quality control applications
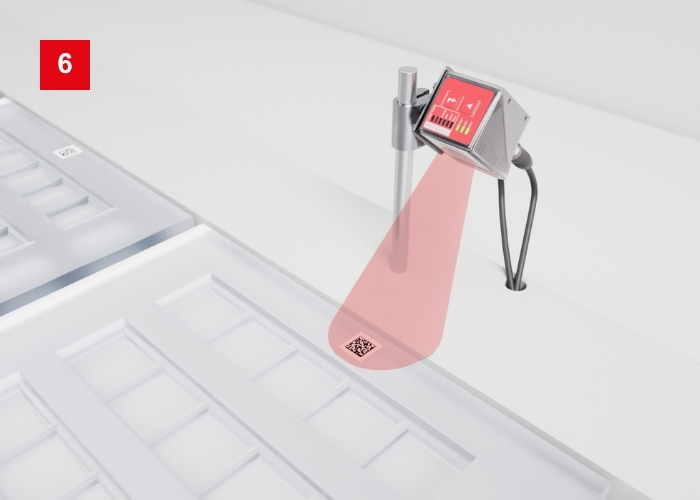
Identification of empty molds
Requirement:
In confectionery production, molds are used to manufacture or mold products. In the process, the first step is to identify and verify the empty mold.
Solution:
The universal compact DCR 200i code reader reliably captures 1D or 2D codes. It is available with a stainless steel housing for use in food processing. For larger distances to the empty mold, the high-performance DCR 1000i Simple Vision sensor is suitable.
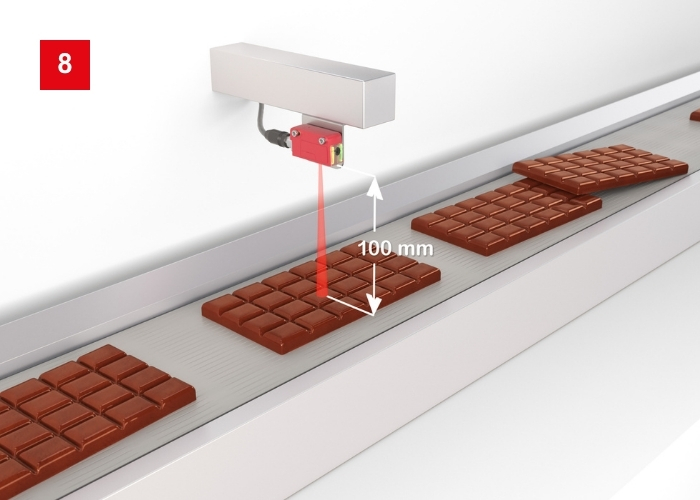
Quality and object height verification
Requirement:
For further processing in a horizontal packaging machine, it is necessary to ensure that the manufactured products (e.g., chocolate bars) move individually along the conveyor belt. To do this, the system monitors whether the defined product height (e.g., objects stacked on top of one another) is maintained.
Solution:
The ODT 3C distance diffuse sensor is installed above the conveyor belt, looking down at the products. It detects the objects (switching sensor function) and simultaneously measures their height (measuring sensor function). This ensures that products run separately on the conveyor belt. The measurement data is output via the IO-Link interface of the sensor.
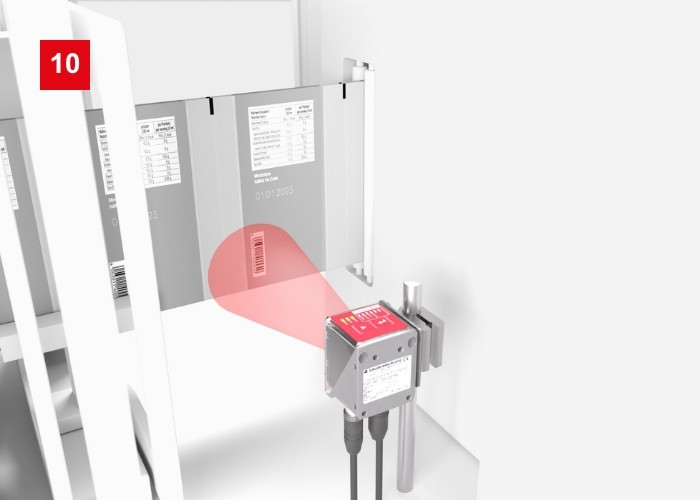
Code identification on flowpacks
Requirement:
In packaging processes, an attached code must be used to ensure that the packaging material and product are correctly assigned. Sensors must control different types of codes and the readability of the code. A camera-based code reader can be used for this purpose.
Solution:
The camera-based DCR 200i code reader decodes 1D- and 2D-codes. With the aid of the integrated reference code function, the sensor can compare the read code with the reference or target code. The result is output in real-time via digital IOs. Alternatively, the code content can be transferred to the machine control via the fieldbus interface.
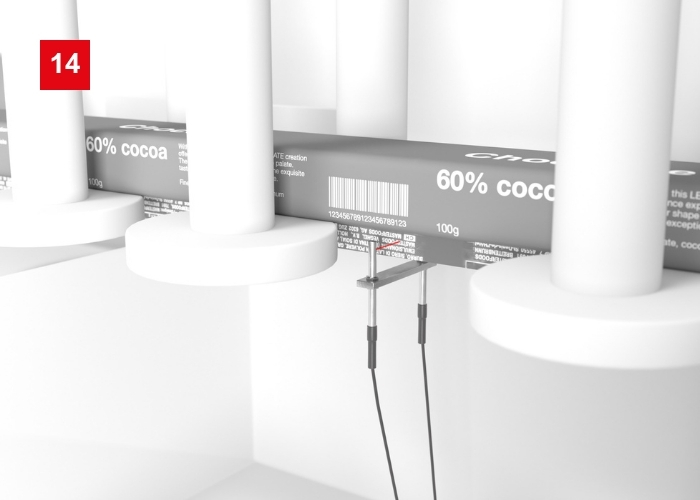
Monitoring of sealed seams
Requirement:
For food packaged in film, a correctly executed sealed seam ensures the shelf life of the packaged products. For this purpose, the sealed seam must be continuously checked in the horizontal process. The sensors used must be adapted to the space available in the machine.
Solution:
The KF and KFX fiber optics with different optical outlets and mounting options can be used flexibly in confined installation situations. When combined with fiber-optic amplifiers such as the LV463.XR, which offer high optical performance, this results in a solution tailored to the application. Further advantages are the analog output and the IO-Link interface.
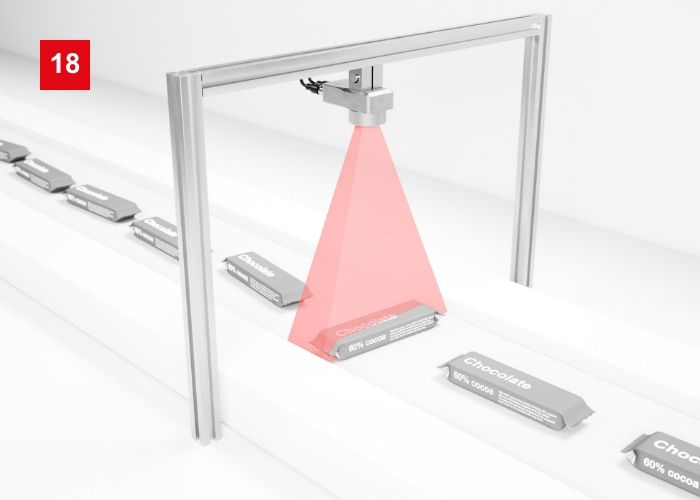
Object alignment inspection
Requirement:
At the outflow of a horizontal packaging machine, the correct alignment of the products must be checked before they are automatically packed into a carton. For this purpose, a camera-based Vision sensor is to be used that looks down on the conveyor belt from above.
Solution:
The IVS 1000i Simple Vision sensor can check the position of the products on the conveyor. The evaluation tools that can be selected in the sensor, e.g. pattern detection or position detection, are used for this purpose. In addition, bar codes or 2D-codes on the product can also be read and checked.
Applications for packaging materials
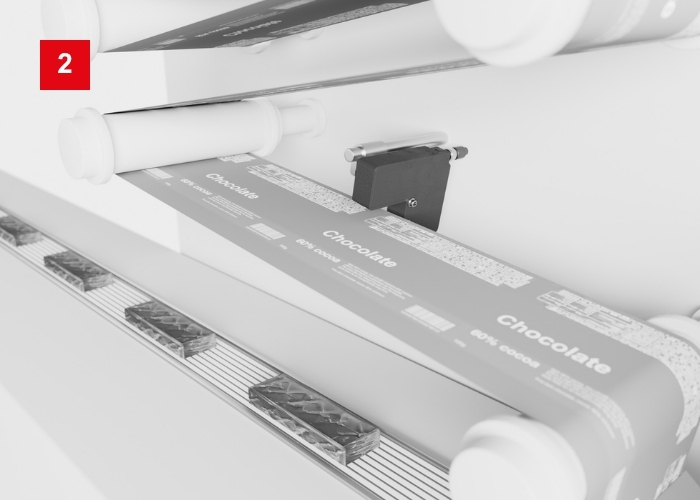
Web edge measurement
Requirement:
To guarantee a parallel film run and right-angled cuts, a web edge control along the film run is helpful. High demands on accuracy require a precise measuring sensor.
Solution:
The GS 754 measuring fork sensor is available in different jaw widths for edge control with maximum precision. The resolution of 0.01 mm allows for very fine web guiding. The GS 754 is a reliable solution for a wide range of materials.
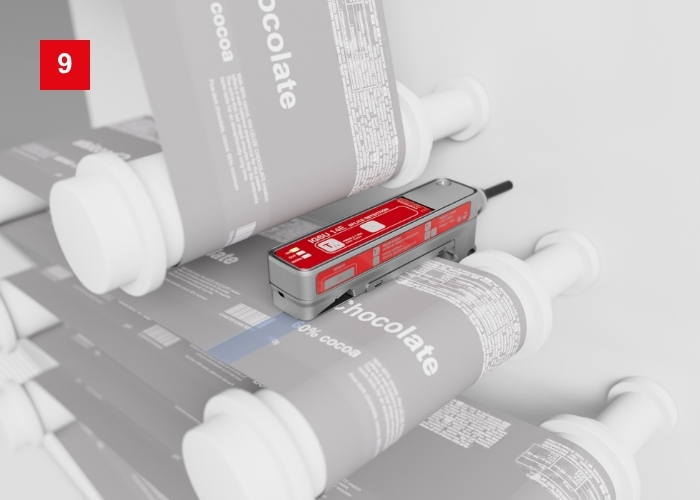
Detection of splices
Requirement:
Splices that occur when changing the packaging film rolls must be reliably detected and discharged in the process. The detection of the splice should be as independent of color and surface as possible, since the printing on the packaging film can vary widely.
Solution:
IGSU14E SD fork sensors reliably detect splices. Due to their ultrasonic principle, they can work with any type of printing. The sensors can be taught quickly and easily using the teach function. A diagnostics function is possible via the integrated IO-Link interface.
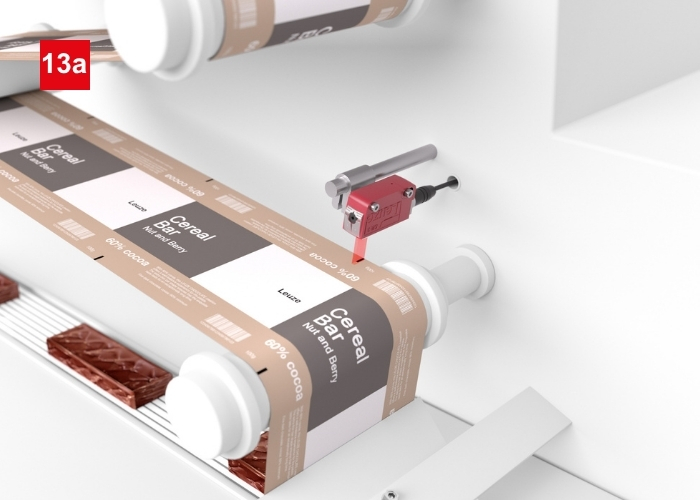
Detection of cut marks in film feed
Requirement:
Products are packed in packaging films in horizontal packaging machines. Sensors must detect the printed contrast markers and thus control the precise cutting process. Common challenges are the limited installation space and the frequent format changeovers due to films and contrast markers of different colors.
Solution:
The compact KRT 3C contrast sensor is available in three models: the flexible version with RGB LEDs, a universal version with white light, and a version for larger distances with laser-generated red light. The sensors can be taught via the integrated teach button, IO-Link, or cable.
Special challenges in the packaging of confectionery and bakery products
Unlike in other industries, the environmental conditions are generally dry and warm, so requirements regarding the sensors’ resistance to cleaning or surface finish are of secondary importance.
Fiber-optic sensors are particularly well-suited for applications in areas with elevated temperatures. In addition, special light spot shapes and sensor technologies that use the background as a reference enable stable and reliable detection – even under difficult conditions.
Another important aspect is content checks. Since primary packaging consists primarily of film – from transparent to metallized versions – sensors must be able to reliably distinguish between properly filled and incomplete packages.
Sensors with IO-Link also support quick product and format changes through simple configuration. This helps reduce downtime and sustainably increase packaging machines’ flexibility.
Our sensors feature integrated IO-Link interfaces. This allows parameter settings, presets, and product-specific recipes to be transferred directly from the machine control to the sensors. Any necessary adjustments during product or format changes can thus be implemented quickly and easily. This reduces downtime, increases system availability, and enables highly flexible production.
Other topics in the packaging industry
Frequently asked questions about the confectionery and bakery industry
For automation, the machine or process control system must have access to information regarding the position, presence, and possibly other data related to the objects being processed and the transport technology. Sensors and rotary encoders are used for this purpose. Occupational safety must also be ensured at “hazardous” locations.
Key applications include dosing and temperature control in the mixing and raw material processing stages. Later in the process, from the finished raw product through to packaging, applications for presence detection, completeness monitoring, and quantity monitoring during package filling become more common.
The challenges stem from the wide variety of product shapes and colors, as well as the predominantly multi-track system design. This places high demands on the sensors’ mounting positions as well as on their detection capabilities to ensure reliable and safe object detection under all operating conditions.
Since the individual lanes of a multi-track system generally need to be monitored separately, object detection is usually only possible from above or below the conveyor belt. At the same time, products must be reliably detected regardless of their color, shape or surface structure – ideally without the need for reconfiguration when switching products. These requirements call for specially optimized sensors that ensure reliable and stable detection even under changing conditions.