


Sensors for palletizing
The final step in the packaging process, known as end-of-line, involves consolidating, loading, and, if necessary, stacking fully packaged products and packaging units for subsequent transport. In this process, the products are typically aligned automatically and arranged on suitable load carriers – in particular standardized pallets – to form stable and transportable units.
Various factors must be taken into account during the stacking process. These include, in particular, the external dimensions of the products, an optimized layer pattern, balanced weight distribution, and specific local and logistical requirements. Once stacking is complete, the transport unit is secured in accordance with transport requirements to prevent slipping, shifting, or instability during further transport. Stretch film, straps, or similar load-securing systems are typically used for this purpose.
The secured transport unit is then transported via the downstream logistics chain to its respective destination. For efficient and reliable handling of delivery processes – both in retail and in direct shipping to end customers – clear labeling of the transport unit and the complete provision of the required shipping and accompanying documents are of central importance.
Your benefits with our palletizing solutions
Reliable object detection
Reliable object detection using specialized light spot shapes and light bands
Space-saving solution
Reduced space and installation requirements thanks to innovative smart gating in light curtains
Reliable reflection detection
Reliable detection of reflective surfaces using depolarizing filters
Sensor applications in palletizing
In the final packaging step, cartons and packages are stacked onto pallets and then transferred to downstream warehouse and transport logistics. Palletizing involves numerous tasks – from detecting variable object geometries and monitoring the stacking process to checking the external dimensions.
The subsequent securing of the load using straps or stretch film – for example, with film winders – poses additional challenges, particularly with regard to reliable material supply. An efficient and trouble-free material flow, as well as seamless machine safety, are therefore key requirements in the end-of-line area.
Click on the numbered applications to learn more about the respective sensor solutions.
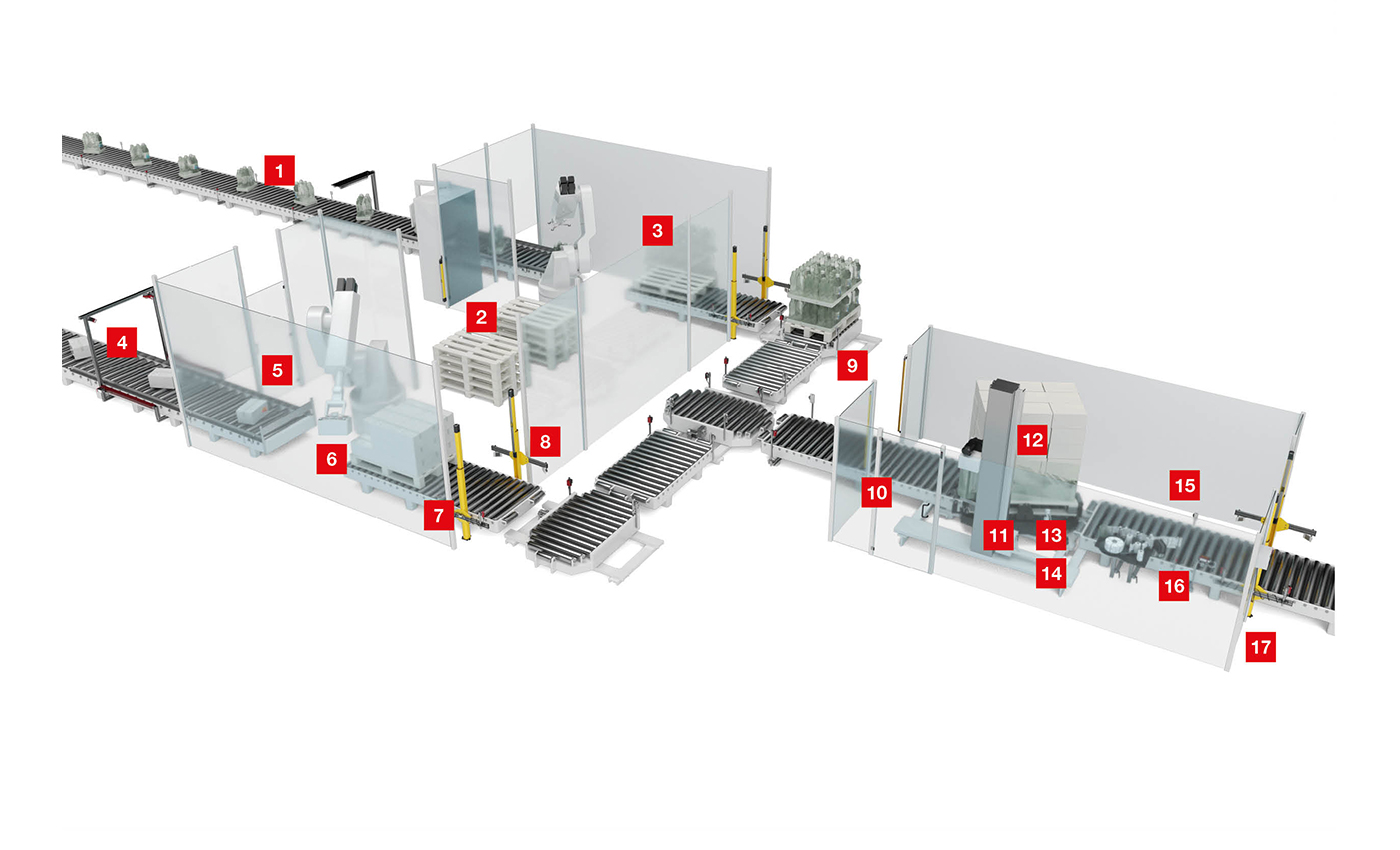
Application areas in the palletizing process
The range of applications includes tasks related to the reliable material provision as the basis for a trouble-free stacking and wrapping process. In addition, there are the control signals required for automated transport, as well as applications for securing the load during transport and for wrapping the finished palletized load carrier in film. The range is rounded out by workplace safety applications.
Applications for wrapping pallets
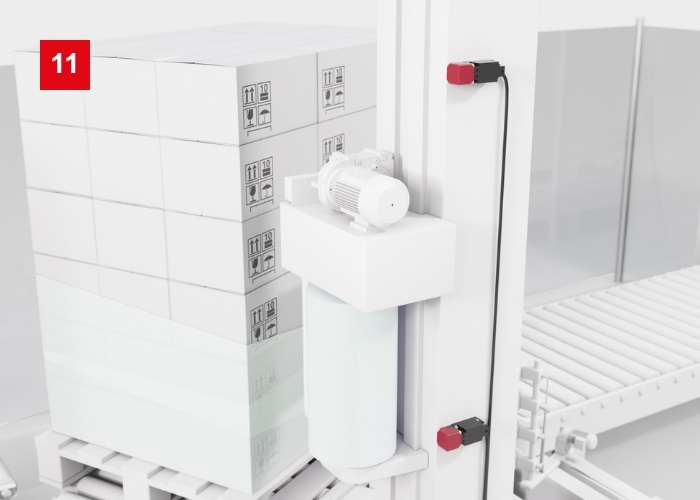
Monitoring of end positions
Requirement:
For transport safeguarding, pallet loads are often automatically wrapped in stretch film. In pallet wrapping machines, the film carriage’s final position must be monitored to prevent collisions.
Solution:
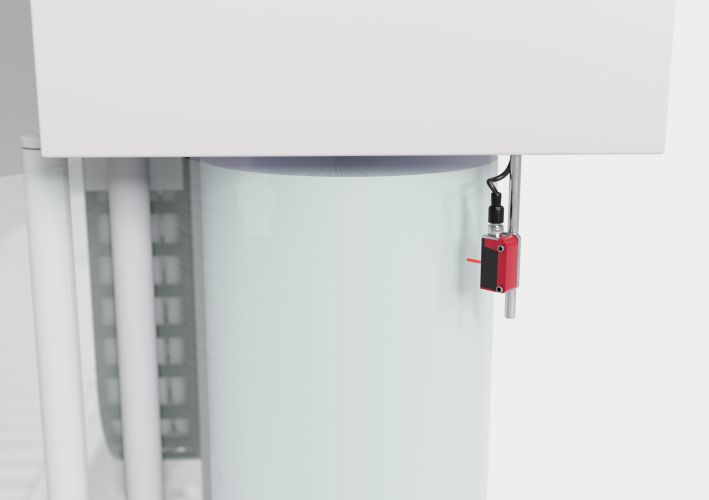
Inductive sensors detect the film carriage based on the metal parts installed on it. These IS 244 cubic inductive sensors with a rotatable active head and a clamp or M12 connection can be mounted flexibly with ranges of up to 40 mm.
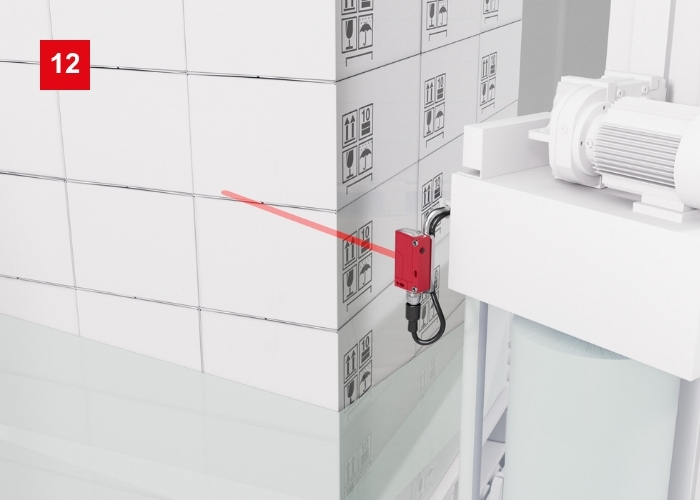
Detection of winding height
Requirement:
For a correct winding process, the pallet’s maximum height must be detected. The upper edge of the pallet must be detected to control the film carriage.
Solution:
The HT 46C diffuse sensor detects the upper edge of the loaded pallet at an operating range of up to 3 m with defined fading independent of the objects on the pallet.
> Learn more about diffuse sensors with background suppression
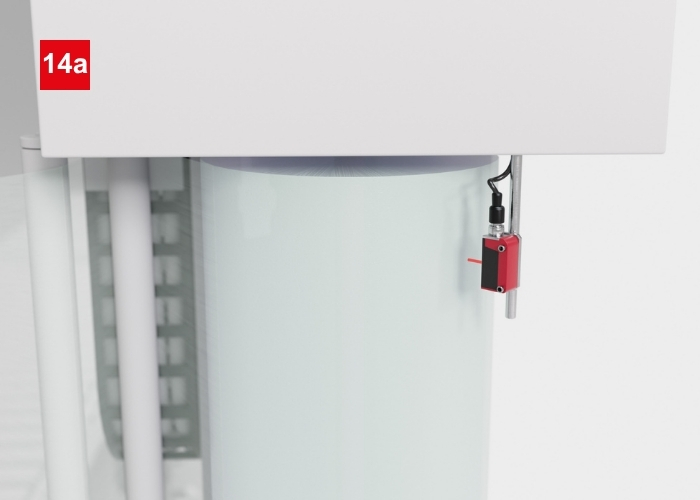
Determination of residual quantities
Requirement:
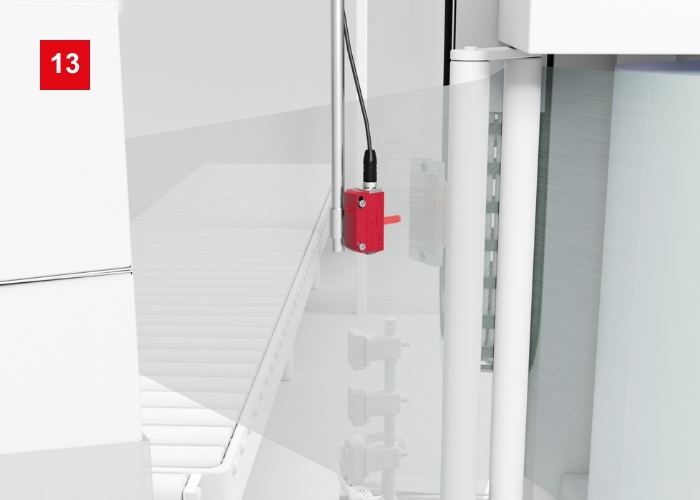
To ensure a reliable winding process, the film supply must be monitored so that a signal is received in a timely manner when a roll change is necessary. A sensor is to be used that can reliably detect the residual quantity independent of the type of film.
Solution:
The HT 3C and HT 25C diffuse sensors with highly visible red light spot allow fast alignment in the machine and detect the film roll independent of color and surface. The sensors can be adjusted either with a potentiometer or via the integrated IO-Link interface.
> Learn more about diffuse sensors with background suppression
Applications in object and pallet transport
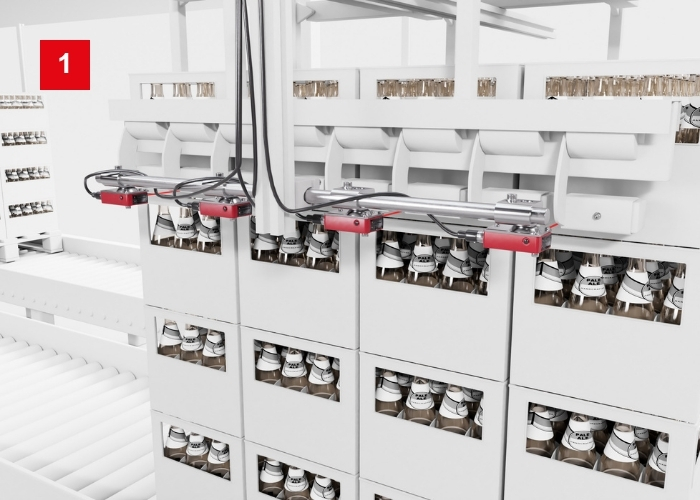
Detection of objects
Requirement:
In the final packaging or palletizing of packages, the presence of objects must be checked. Objects with gaps must also be reliably detected.
Solution:
The RK 46C or PRK 36 retro-reflective photoelectric sensors have a long operating range and thus a very high function reserve. In other models, the sensitivity can be adjusted, and a Depol function increases the availability of the system. All sensors have protection class IP 69K and ECOLAB certification.
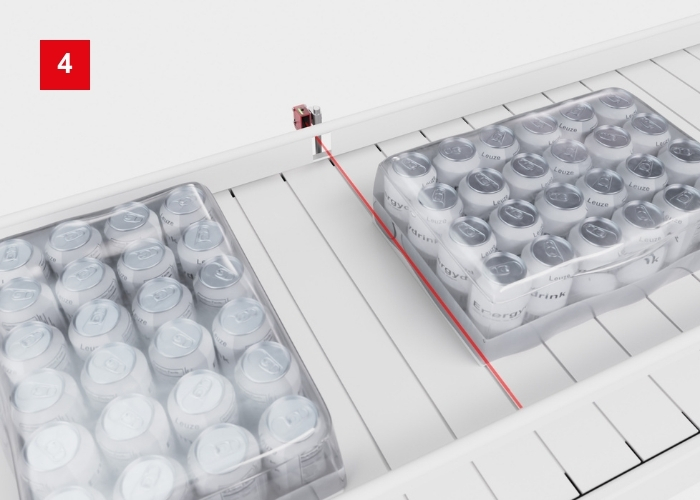
Detection of objects on conveyor belt
Requirement:
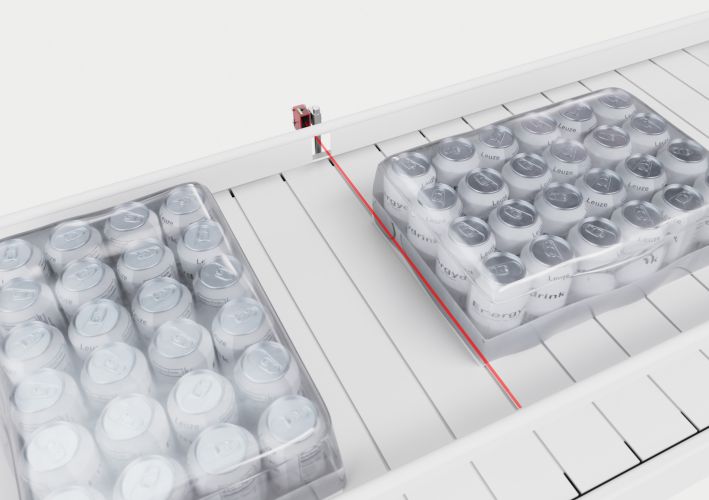
Packages or cartons that are shrink-wrapped with film are transported on a conveyor belt and must be reliably detected.
Solution:
The PRK 15D.D or PRK 25C.D retro-reflective photoelectric sensor is optimized for the detection of shrink-wrapped objects and thus offers a high function reserve. If limited installation space is available, the PRK 5B.D sensors with smaller housing are used.
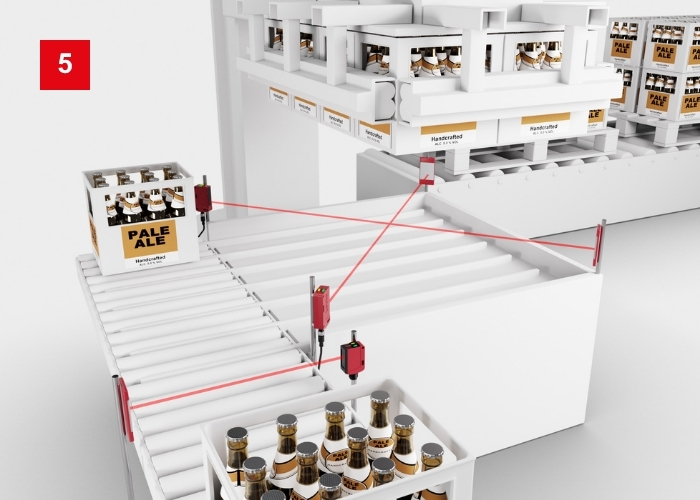
Detection and positioning of objects
Requirement:
Objects must be identified, or their respective stop positions detected, along transport segments or at transfer points. To achieve this, the sensors used must offer good alignment capability and high repeatability. They must also be able to tolerate object variations and any contamination.
Solution:
The detection and positioning of packages can be solved with different retro-reflective photoelectric sensors. Depending on the required performance margin and dimensions, the reflective photoelectric sensors of the 28, 25C or 46C series in a cubic design and the 328 series in a cylindrical design are suitable. All sensors have protection class IP 67 or IP69K and ECOLAB certification.

Detection of pallets from below
Requirement:
Different types of pallets are transported using a pallet conveyor system. To be able to set up the conveyor system segments once they are completed and fully installed, the pallets must be detected from below. High-frequency LED hall lighting or dust particles must not interfere with the sensor.
Solution:
The SET-HT25CI mounting system combines a special holder with a HT 25C diffuse sensor. The holder has an integrated front screen positioned at an angle so that any falling dirt particles are deflected automatically. The special parameterization of the sensors efficiently suppresses potential ambient light sources.
> Learn more about diffuse sensors with background suppression
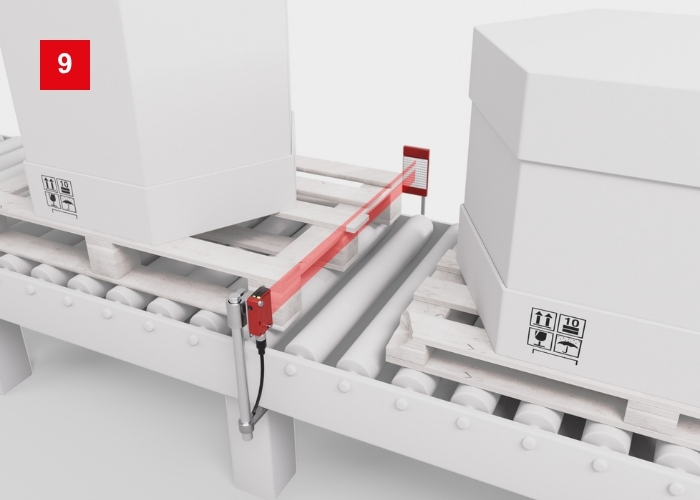
Detection of pallets
Requirement:
All types of pallets must be reliably detected along their entire length. Damaged pallets or pallets with irregular front edges must also be accepted.
Solution:
The RK 46C retro-reflective photoelectric sensors also reliably detect objects with irregular shapes and openings. For this purpose, the devices use a homogeneous, clearly visible 40 mm wide light-band and a standard TKS50x100 reflector. The sensors can be adjusted quickly and easily using a teach button.
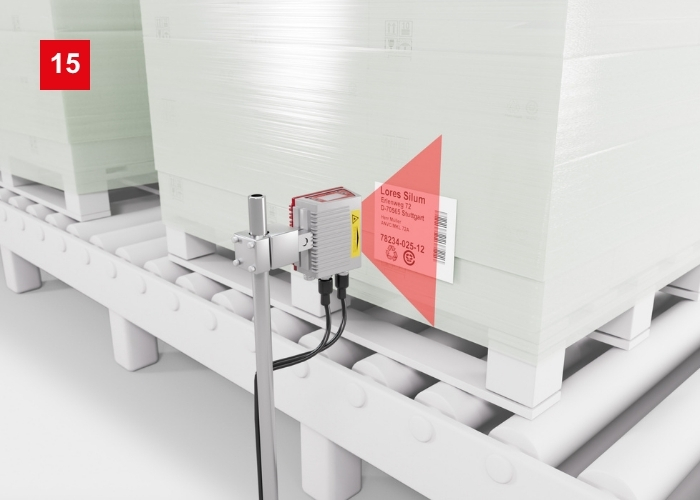
Code reading on the pallet
Requirement:
After palletizing and successful load securing, the goods code on the attached bar code labels must be read in and transferred to the higher-level goods management system.
Solution:
A bar code reader of the BCL 500i / BCL 600i series is used to read the pallet label. The integrated fieldbus connectivity is one of the key features of this series and enables quick connection to various control systems. The CRT technology enables damaged codes to be read reliably.
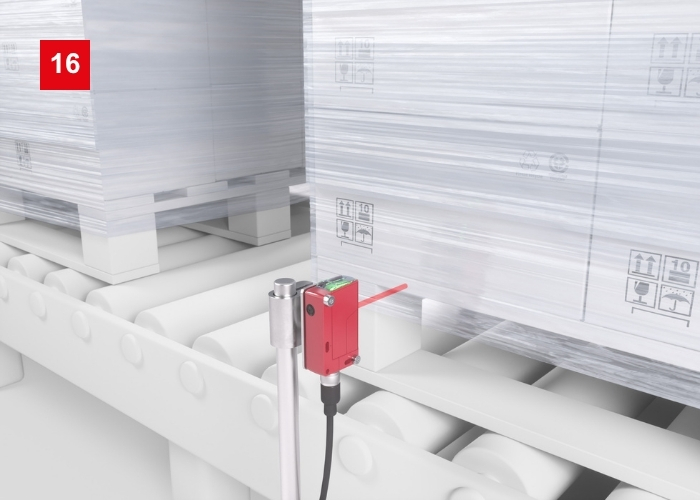
Detection of wrapped pallets
Requirement:
The film- or shrink-wrapped pallets should be reliably detected along the entire pallet length. The sensor used must not generate any switching errors.
Solution:
The PRK 36.D, PRK 46C.D and PRK 25C.D retro-reflective photoelectric sensors are optimized for use on roller conveyors. They offer high functional reliability especially for film- and shrink-wrapped pallets. The sensors with protection class IP 69K are mechanically very robust and very reliable due to their high function reserve and operating range of up to 16 m.
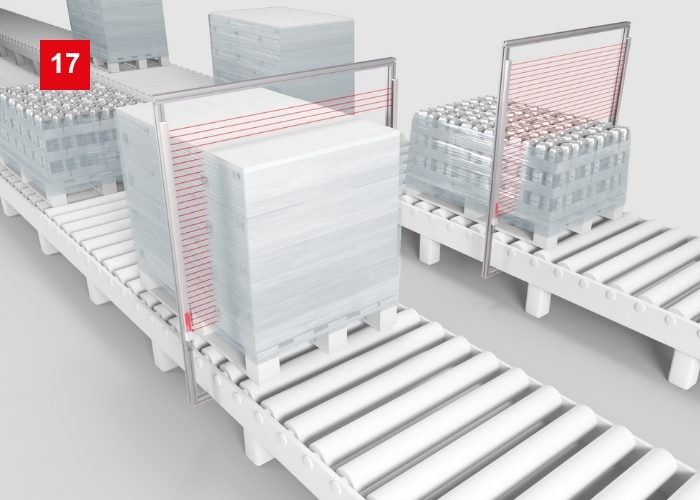
Width and height verification
Requirement:
Before a loaded pallet can be conveyed into the conveyor system or into an automatic storage system, the external dimensions and any projecting edges of the pallet must be checked.
Solution:
The CSL 710 switching light curtains or the CML 720i measuring light curtains check the dimensions of the loaded pallet during transport. Different resolutions and measurement field lengths as well as several configurable outputs allow the devices to be optimally adapted to the application.
Applications for packaging materials
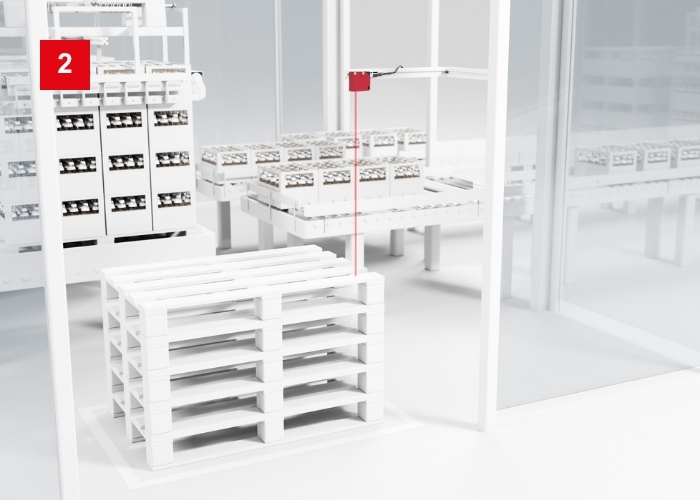
Height measurement of pallet stacks
Requirement:
In an automated palletizing process, it must be ensured that sufficient empty pallets are available in a buffer. For a reliable process, the stack height of the pallets must be monitored for this purpose.
Solution:
Optical measuring sensors ensure reliable height measurement. The ODS 110 distance sensor can output the distance either via an analog value or the integrated IO-Link interface. Thanks to the small, clearly visible class 1 laser spot, the sensor is safe for the eyes and easy to position.
Monitoring pallets
Requirement:
When standard pallets are used, the condition of each pallet is to be checked before it is used again. Among other things, it is necessary to check whether the running boards as well as the pallet blocks are present.
Solution:
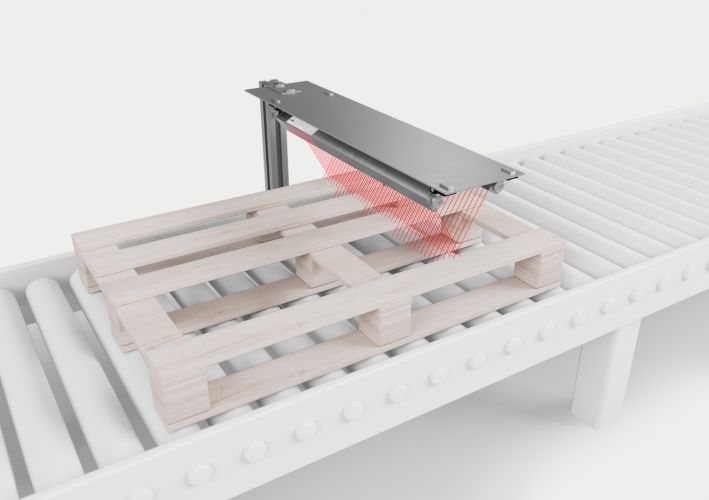
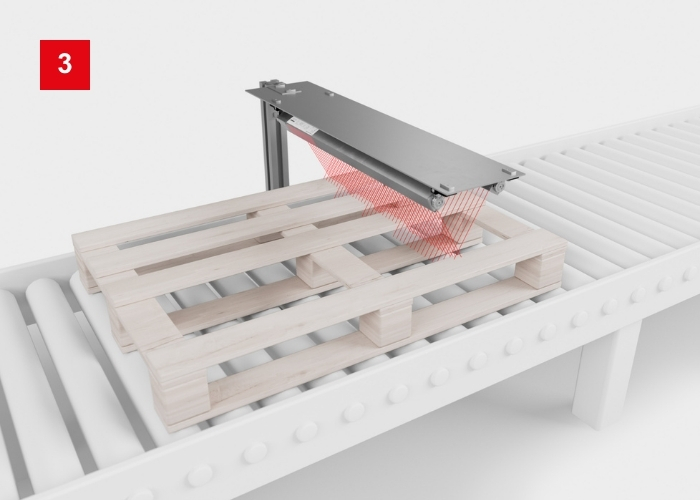
With the aid of the single-beam evaluation of the CML 730i measuring light curtains in V-arrangement, the running boards can be detected and evaluated. The sensor array detects any gaps or missing boards and thus enables defective pallets to be removed early on.
Detection of film
Requirement:
During the winding process, the presence of the film used must be monitored. Any film tears that occur must be reliably detected. A suitable sensor is important for detecting the often transparent or partially transparent film.
Solution:
The polarized PRK 3C.A or PRK 25C.A retro-reflective photoelectric sensors are suitable for the detection of transparent films. The integrated IO-Link interface provides extensive diagnostic options as well as the possibility to parameterize the devices remotely. MTKS reflectors or REF6 reflective tapes are used as reflectors.
Applications in the safety sector
Access guarding with muting
Requirement:
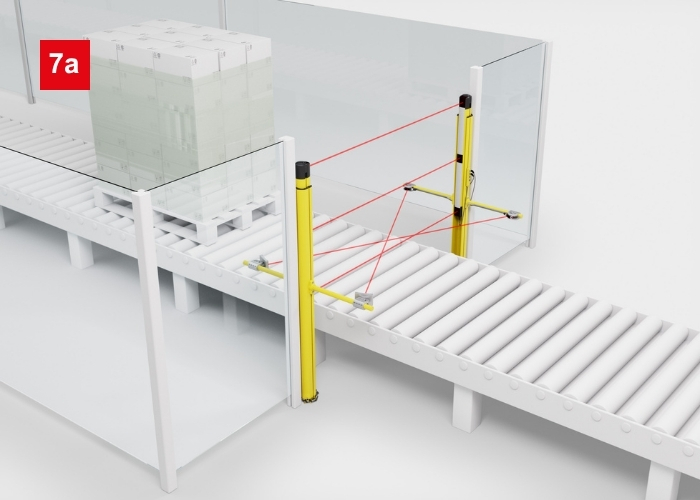
Access guarding on conveyor lines is to prevent persons from accessing a potential danger zone, while at the same time allowing the transported goods to pass through.
Solution:
The muting function bridges the safety sensor during the passage of the transported goods. This function is already integrated in the MLD 530 multiple light beam safety devices and the MLC 530 safety light curtains. The MLD-SET protective sensor sets offer complete solutions for access guarding with muting function.
Access guarding on the palletizer
Requirement:
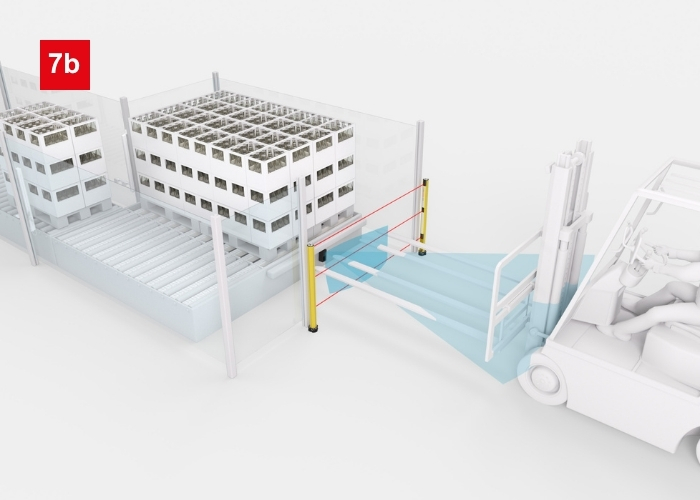
Pallet groupers / ungroupers must be guarded against access by persons. This requires reliable distinction between persons and the manually operated forklift trucks. To simplify the workflow and to minimize interruptions, an automatic system restart must be possible.
Solution:
The safety solution combination: Access is secured by an MLD multiple light beam safety device. A sensor for detecting the forklift truck is installed behind this. By evaluating the sensor signals and their sequence, the safety system distinguishes between forklift trucks and persons. Automatic restart is possible.
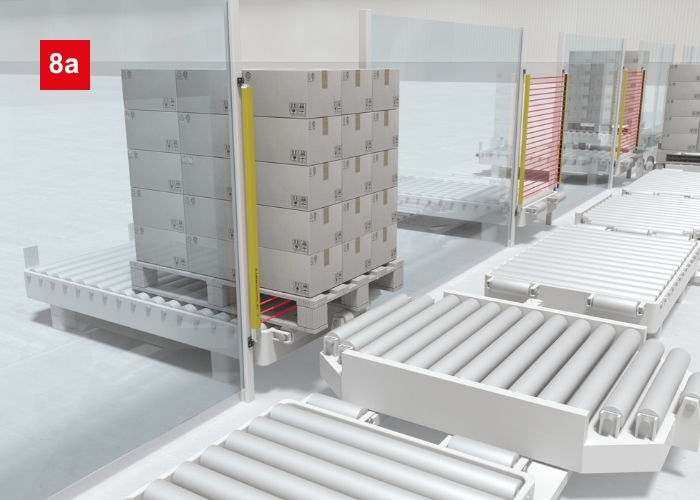
Access guarding with Smart Process Gating
Requirement:
Access guarding on a conveyor line must prevent persons from accessing a potential danger zone, while at the same time allowing transported goods to pass through. Ideally, the safety technology used for this requires as little space as possible.
Solution:
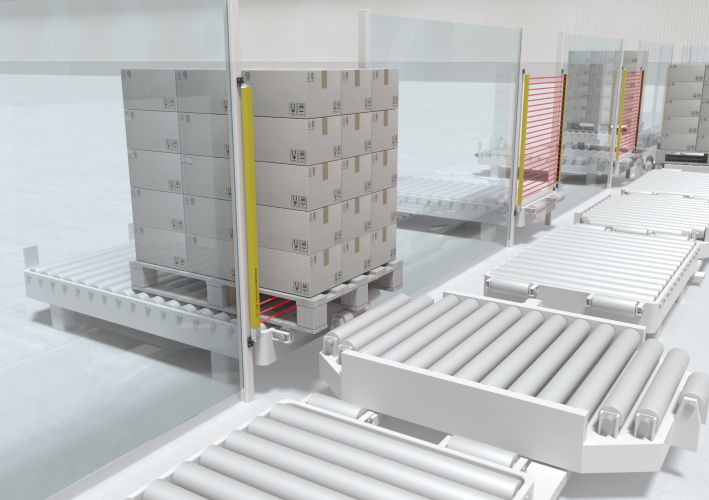
With Smart Process Gating, the safety sensor is bridged by means of a control signal from the PLC. The function is integrated in the MLC 530 SPG safety light curtain. Additional muting sensors are not required and the systems can be designed to be particularly space-saving as well as tamperproof thanks to the SPG function.
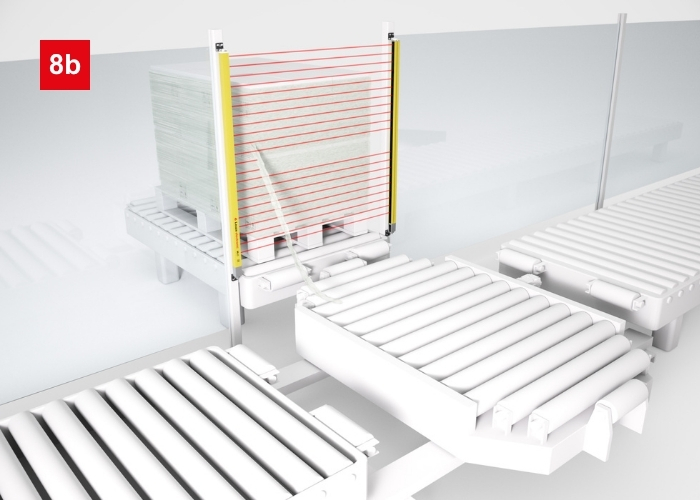
Access guarding with film tolerance
Requirement:
The access guarding system must prevent people from entering a potential hazard area despite the presence of film strips resulting from the wrapping process. Ideally, this is a variation of the space-saving safety technology used.
Solution:
With the reduced resolution, narrow film strips that interrupt up to two adjacent beams can be tolerated using the Smart Process Gating function in the MLC 535-SPG RR safety light curtain without compromising safety.
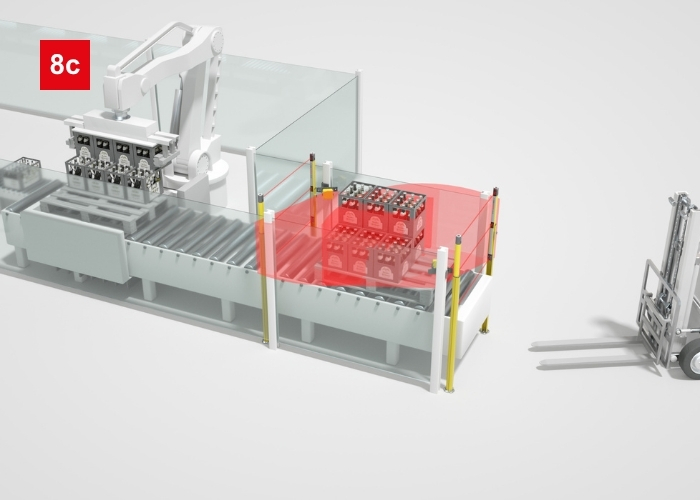
Access guarding at the transfer station as a solution
Requirement:
The robot cell is fed automatically. The material is loaded onto the conveyor line, e.g. using a forklift truck, and then transported into the cell. Access to the cell must be safeguarded. To guarantee optimum capacity utilization of the robot cell, the safety concept must also allow uninterrupted operation of the cell during loading.
Solution:
The loading area of the conveyor line is guarded at both the feed and outfeed side by multiple light beam safety devices. The area between the photoelectric sensors is monitored for the presence of persons by safety radar sensors. The integration is carried out using a specifically developed solution.
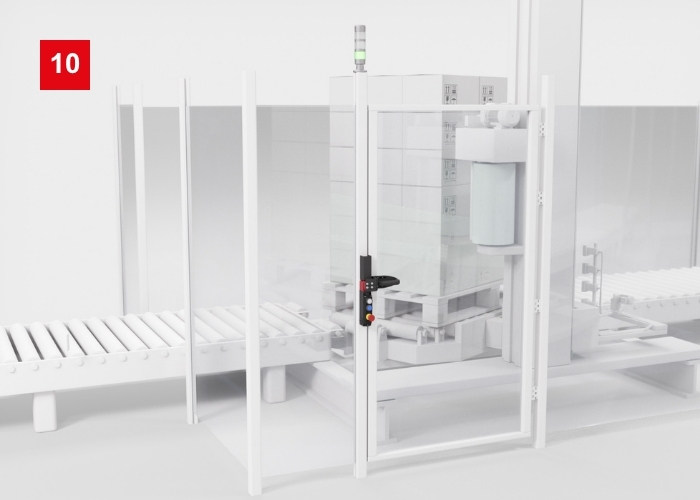
Access guarding of doors
Requirement:
Areas with hazardous movements can be entered via protective doors to allow maintenance. If the movement does not stop immediately after the door is opened, the door is to be guarded by a safety switch with guard interlocking.
Solution:
The robust L100, L250 and L300 safety switches with guard interlocking keep protective doors securely locked until access is released by an electric signal. The series includes standard designs, devices with integrated operational controls as well as devices with RFID‑coded actuators.
Other topics in the packaging industry
Frequently asked questions about palletizing
Cartons or containers stacked with their outer edges aligned must be securely fastened to prevent them from sliding or falling during subsequent transport. A common method is to secure them with taut stretch or shrink film, which is wrapped around the cartons and, in some cases, around the pallet as well.
For sturdy cartons and lighter products, tensioned plastic straps are used as an alternative. These are wrapped around the package both lengthwise and crosswise depending on the requirements. For fragile goods, corner protectors can also be attached to the corners. These protect the packaging and also help ensure the stability of the load.
Pallet stability is of critical importance. Both in the warehouse and in transport logistics, a tipped-over pallet can lead to significant operational disruptions and damage. In many sectors that use standardized pallets, rental and exchange systems are also in place, whereby full pallets are delivered and empty pallets returned.
However, repeated pallet cycle use takes its toll. Therefore, it is important to inspect the condition of the pallets before using them again. This involves checking whether the pallet is complete, stable, and undamaged – in particular, whether all the planks and feet are present and intact.
In automated palletizing and pallet wrappers, both the film supply and the movement paths of the components involved, such as the wrapping arm or the pallet clamping mechanism on turntables – must be reliably monitored. Suitable sensor solutions are used here to ensure safe and trouble-free process control.
So-called muting sensors are used for material transport into a secured area. They allow the safety function to be selectively disabled while material is being loaded or unloaded, without compromising personnel safety. To do this, the muting sensors must be positioned at a suitable distance in front of the safety sensor and controlled accordingly by the control system.
Under defined conditions and in combination with suitable safety sensors, additional muting sensors are not required. The MLC SPG, for example, enables sensorless muting to be implemented while ensuring safety. The space saved as a result facilitates both retrofit projects and the planning of new systems and enables more compact system integration.